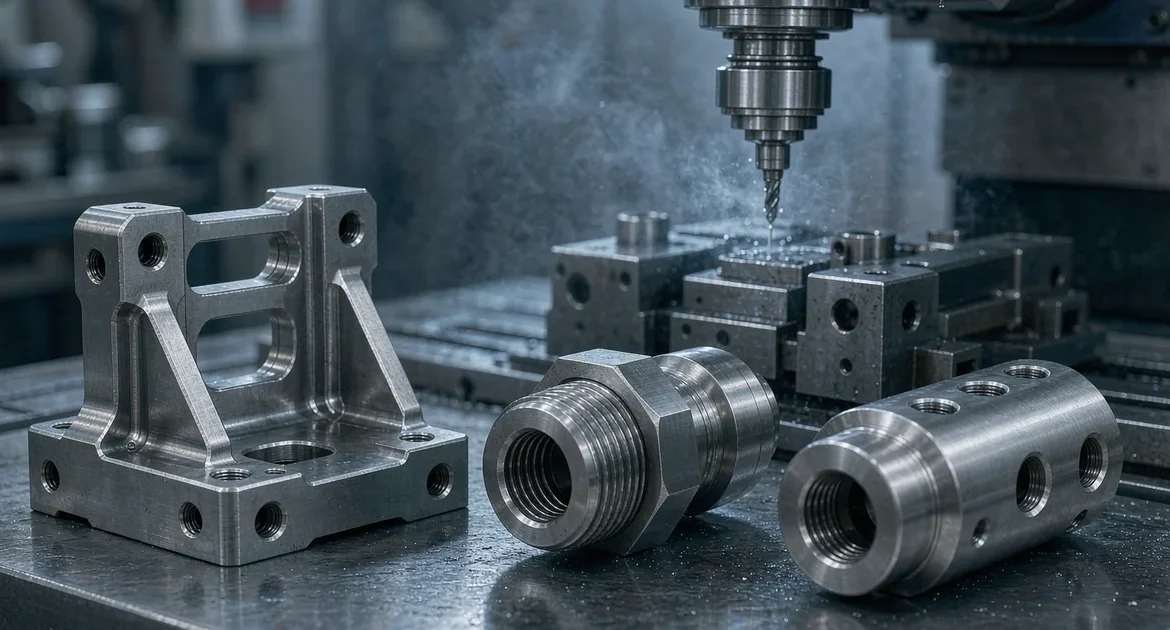
Titanium earns its reputation every time a machinist touches it. It is strong, light, and corrosion-resistant — and it fights back with low thermal conductivity, a tendency to work-harden, and a habit of chewing through cutting tools. Titanium CNC machining is not harder because the material is mysterious; it is harder because the material refuses to cooperate with the shortcuts that work so well on aluminum and steel.
This guide explains the titanium grades that matter for machined parts, why the material behaves the way it does under the cutter, the finishing options that protect and color it, and the design habits that keep titanium parts manufacturable. It is written for engineers and buyers who specify high-performance parts in aerospace, medical, motorsport, and industrial applications.
Why Titanium Is Hard to Machine
Titanium concentrates heat exactly where you do not want it. Its thermal conductivity is a fraction of aluminum’s, so the heat generated at the cutting edge does not flow away into the chip and the workpiece — it stays in the tool. The result is a cutting edge that degrades rapidly, a workpiece that work-hardens if the feed is too light, and a finish that suffers the moment tool wear sets in.
Three behaviors define titanium machining:
- Heat stays local — Poor heat dissipation concentrates temperature at the cutting edge, so titanium is machined at lower surface speeds than aluminum or steel, with generous coolant to carry heat away.
- Work hardening — A dull tool or a light finishing pass can harden the surface mid-cut, making the next pass more difficult and shortening tool life dramatically.
- Springback — Titanium deflects elastically more than steel, so thin walls and long unsupported features require rigid fixturing and conservative cutting parameters to hold size.
Titanium Grades for CNC Machined Parts
Titanium is specified by grade — a designation system maintained by organizations like ASM International — and the grade changes the machining behavior as much as it changes the mechanical properties. The four grades below cover most machined-part work:
| Оценка | Also Known As | Характеристика | Типичное применение |
|---|---|---|---|
| Grade 2 | Commercially pure (CP) | Excellent corrosion resistance, formable, lower strength | Chemical, marine, medical housings |
| Grade 5 | Ti-6Al-4V | High strength-to-weight, the workhorse alloy | Aerospace, motorsport, implants |
| Grade 23 | Ti-6Al-4V ELI | Higher purity, superior fracture toughness | Medical implants, critical aerospace |
| Grade 7 | Ti-0.2Pd | Superior corrosion resistance in acidic media | Chemical processing equipment |
Grade 5 (Ti-6Al-4V) is the default for most structural parts — it balances strength, weight, and cost better than any other titanium. Grade 2 is the choice when corrosion resistance matters more than strength and the part does not need the alloy’s extra performance. Grade 23 is essentially Grade 5 with tighter control over impurities, specified where fatigue life and fracture toughness are critical, such as load-bearing implants. Grade 7 adds palladium for the most aggressive chemical environments.
Machining Strategy: Tools, Speeds, and Coolant
Machining titanium well is a discipline of parameters, not heroics. The approach that works on aluminum will destroy a titanium tool in minutes:
- Coated carbide tooling — Titanium demands sharp, heat-resistant edges. Coated carbide is the standard; the coating reduces heat transfer into the tool and resists the chemical reactivity that welds chips to the edge.
- Lower speeds, higher feeds — The opposite of aluminum. Running slow keeps heat down, while a healthy feed keeps the tool cutting and prevents the rubbing that work-hardens the surface.
- Generous coolant — High-pressure coolant flushes heat and chips away from the cut zone. Dry or mist machining of titanium is asking for a burned tool.
- Rigid fixturing — Titanium’s springback punishes flimsy setups. Short tool overhang and solid workholding keep the part from vibrating out of tolerance.
Tool life is the hidden cost in titanium machining. A shop that has not tuned its parameters for titanium will quote it incorrectly, either losing money or pushing the risk onto the customer through rushed cuts and surface defects. Experience with the material is the difference between a titanium part that meets spec and one that arrives looking fine but fails in fatigue.
Surface Finishing for Titanium Parts
Titanium finishes are driven by function — corrosion protection is largely built in through the natural oxide layer, so finishing is about wear, appearance, and, in medical and aerospace work, surface integrity:
- Анодирование — Titanium anodizing is thinner than aluminum anodizing and is used more for identification and color coding than for heavy wear protection. The voltage controls the color, producing blues, purples, and golds without dyes.
- Пассивация — A chemical treatment that cleans and thickens the protective oxide layer, removing surface iron and improving corrosion resistance. Standard practice for medical and aerospace parts.
- Дробеструйная обработка — Produces a uniform matte finish and can improve fatigue resistance by imparting beneficial compressive stress on the surface, which is why it is common on aerospace components.
- Полировка — Mechanical polishing to a reflective or satin finish for cosmetic parts, frequently specified on visible medical devices and consumer titanium products.
Design Tips for Machinable Titanium Parts
Good titanium design respects the material’s reluctance to cooperate:
- Avoid thin, unsupported walls — Titanium springs back, so a thin wall that holds size in aluminum will wander in titanium. Add thickness or stiffening where the geometry allows.
- Keep internal corners generous — Sharp corners concentrate both stress and machining difficulty. A radius that matches standard tooling reduces tool load and improves fatigue life at the same time.
- Design for tool access — Deep pockets and recessed features force long, flexible tools that titanium punishes. If a feature must be deep, expect the tolerance to loosen or the cost to climb.
- Specify finish intent early — Whether the part needs anodizing, passivation, or bead blasting changes the machining and cleaning sequence. Tell the shop before it cuts, not after.
How GRAN Machines Titanium
At GRAN INDUSTRIES SDN. BHD., titanium is machined with the same first principle we apply to every material: review the drawing before we quote. Material grade, tolerance feasibility, finish intent, and quantity are confirmed up front, because a titanium part quoted on bad assumptions is an expensive mistake for everyone involved.
We machine titanium alongside stainless steel, aluminum, carbon fiber, and engineering plastics, and we keep forging, stamping, sheet metal, and cold heading in-house. That breadth matters for titanium programs, where a near-net forged or formed blank can remove the most expensive machining before a single chip is cut. See our обзор процесса обработки с ЧПУ для полного рабочего процесса от чертежа до поставки.
Start Your Titanium CNC Machining Project
Titanium rewards a shop that respects it and punishes one that treats it like aluminum. If your project calls for titanium parts — aerospace brackets, medical implants, motorsport components, or corrosion-critical hardware — send your drawing, reference sample, or project brief to info@gran.my или позвоните по телефону +60 10-881 2868. Укажите марку материала, объём, допуски и требования к обработке поверхности, и мы рассмотрим проект и вернём котировку с рекомендуемым маршрутом обработки и сроками поставки. Ознакомьтесь с нашими полными возможностями на gran.my.
Часто задаваемые вопросы
Q: What titanium grades can you machine?
A: We machine the grades that cover most CNC work — Grade 2 (commercially pure), Grade 5 (Ti-6Al-4V), Grade 23 (Ti-6Al-4V ELI), and Grade 7, among others. Grade 5 is the default for structural parts, Grade 2 for corrosion-driven applications, Grade 23 where fatigue life and fracture toughness are critical, and Grade 7 for aggressive chemical environments. Share your operating conditions and we will recommend the right grade during quotation.
Q: Why is titanium harder to machine than steel or aluminum?
A: Titanium conducts heat poorly, so the heat of cutting stays concentrated at the tool edge instead of flowing away with the chip. It also work-hardens if the feed is too light or the tool dulls, and it springs back elastically more than steel. Together these force lower cutting speeds, sharper coated-carbide tooling, generous coolant, and rigid fixturing. A shop experienced with titanium sets parameters very differently from one used to aluminum.
Q: What surface finishes are available for titanium parts?
A: The main options are anodizing (thin, used for color coding and identification), passivation (cleans and thickens the protective oxide for corrosion resistance), bead blasting (uniform matte finish that can also improve fatigue life), and polishing for cosmetic parts. The right choice depends on the part’s function — medical and aerospace parts typically require passivation, while visible consumer products often get anodizing or polishing.
Q: What tolerances can you hold on titanium CNC parts?
A: With rigid fixturing and tuned parameters we routinely hold around ±0.05 mm on general titanium features and tighter on critical diameters with the right setup. Titanium’s springback means thin walls and long unsupported features force tolerances open more than they would in aluminum or steel, so achievable numbers always depend on geometry. Critical dimensions are verified by measurement and documented in inspection reports.